Repair & Overhaul: Hydraulic Cylinders
Repair & Overhaul: Hydraulic Cylinders
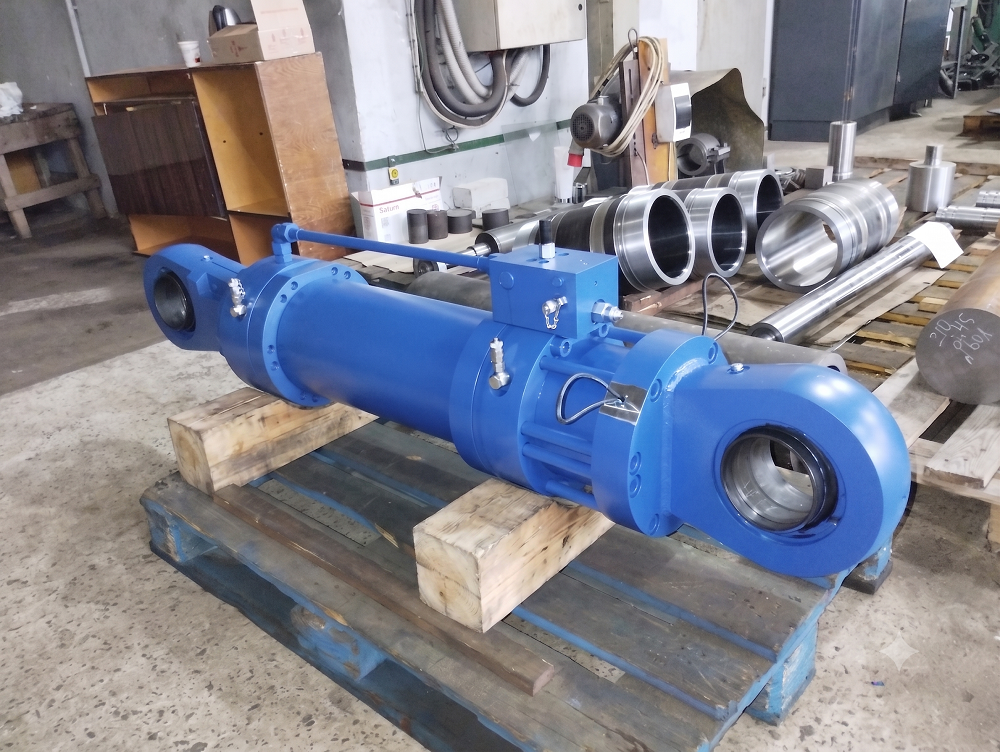
Overhaul and remanufacturing of heavy industrial hydraulic cylinders up to Ø 700 mm bore and 6,000 mm length. Complete diagnostics, geometric reconditioning, new component machining and hydrostatic pressure testing.
Cylinder Types Handled
Cylinder Configuration
Remanufacturing & Repair Operations
- Double-Acting Industrial Cylinders
Piston and rod seal replacement, guide bush renewal, barrel honing/re-boring, rod re-chroming or fabricating brand-new piston rods.
- Single-Acting & Plunger Cylinders
Plunger re-grinding, hard chrome plating, multi-lip chevron packing replacement and gland bush remachining.
- Multi-Stage Telescopic Cylinders
Restoration of nested plunger stages, internal inter-stage seal pack replacement and precision stage straightening.
- Heavy Heavyweight & Mill-Duty Cylinders
Remanufacturing oversized tie-rod, welded and mill-type cylinders for steel plants, mining excavators and forging presses.
Why Choose Us for Hydraulic Cylinder Repair
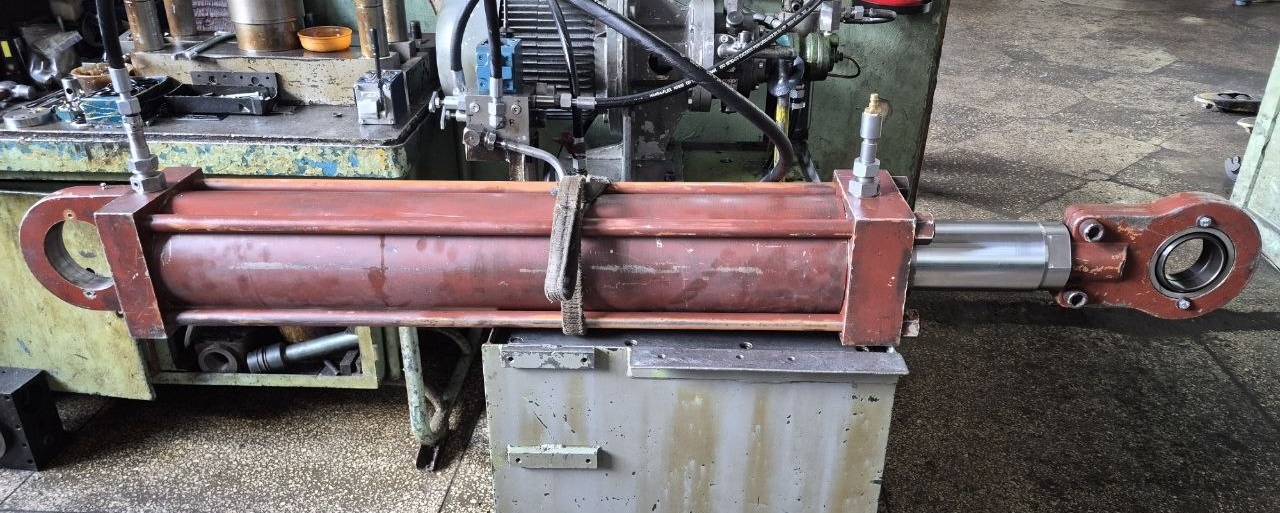
- We repair cylinders with bore sizes up to Ø 700 mm and lengths up to 6,000 mm. Few service facilities have the machinery and handling equipment required for units of this scale.
In-House Reconditioning and Machining Fleet
- Our comprehensive fleet of turning, boring, and grinding machines, along with a dedicated weld cladding section, allows us to recondition worn components (piston rods, cylinder barrels, guide bushes) rather than resorting to costly full assembly replacements.
Dedicated Test Benches
- Every overhauled cylinder undergoes rigorous proof testing under full hydraulic load. We issue an official technical passport (test certificate) detailing actual measured performance parameters.
12-Month Warranty
- A full 12-month warranty covering all repair and remanufacturing work performed.
Step-by-Step Cylinder Overhaul Procedure
01
Diagnostics and Defect Analysis
- Incoming inspection and exterior cleaning of the cylinder
- Geometric verification of the piston rod, cylinder barrel, and mounting eyes (clevises/trunnions)
- Test bench evaluation to detect internal cross-port leakage
02
Disassembly and Cleaning
- Complete teardown of the hydraulic cylinder
- Thorough cleaning of all components to remove contamination and degraded oil/grease
- Chemical flushing of internal fluid chambers
03
Machining and Component Restoration
- Cylinder barrel boring — restoring the bore geometry and surface finish of the tube (diameters up to Ø 700 mm, lengths up to 2,000 mm; available for oversize repair dimensions or subsequent sleeve insertion)
- Piston rod cylindrical grinding — restoring rod surface geometry (diameters up to Ø 400 mm, lengths up to 2,000 mm), followed by hard chrome plating as required
- Weld overlay (cladding) of piston rods — repairing surface wear, gouges, or scoring (diameters up to Ø 400 mm, lengths up to 2,000 mm), followed by CNC finish turning (swing up to Ø 1,000 mm, lengths up to 5,000 mm) and finish cylindrical grinding
- Fabrication of guide bushings and wear rings — precision CNC turning from bronze, brass, or steel
- Thread reconditioning — chasing or re-cutting damaged threads on the rod end or cylinder barrel
- Restoration of mounting eyes and lugs — milling and precision coordinate boring of pin and spherical bearing bores (up to Ø 250 mm, boring depths up to 750 mm)
- Custom component fabrication — precision CNC machining of custom parts and fittings
04
Component Replacement
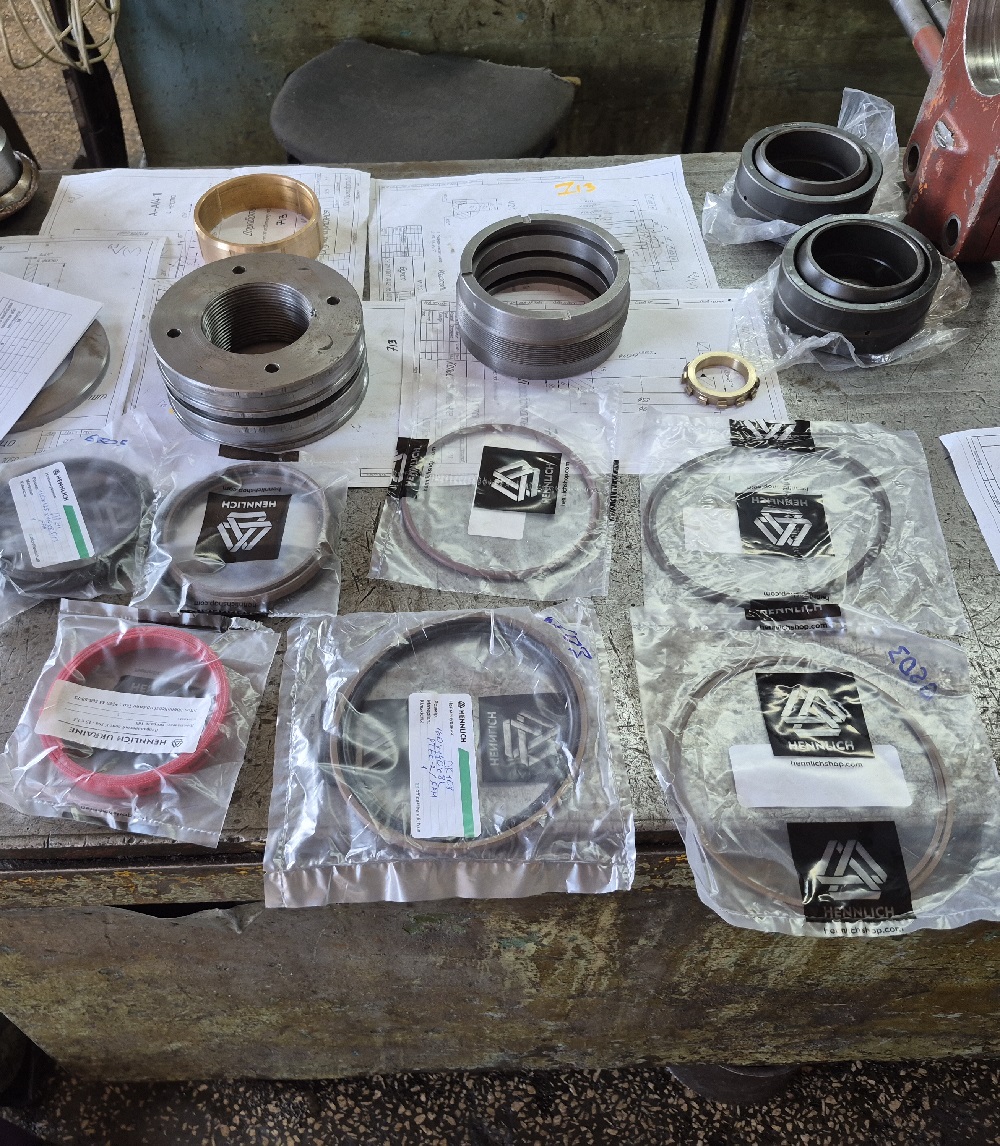
- Seal packages (rod seals, piston seals, wear rings, wiper/scraper rings) — genuine OEM or high-performance certified equivalents
- Guide bushings and bearings (bronze, polyamides/cast nylon, steel)
- Pistons (if beyond repairable tolerances)
- Complete rod assemblies (in cases of critical structural fatigue or catastrophic damage)
- Cylinder barrels/tubes (if boring or honing is unfeasible)
05
Assembly and Calibration
- Verification of axial and radial fit clearances
- Controlled assembly adhering strictly to specified tightening torques
- Setting and tuning of end-of-stroke cushion throttles / deceleration dampers (if equipped)
06
Test Bench Validation
- Static and dynamic proof testing under rated working and peak pressures
- Verification of smooth stroke extension/retraction with zero binding or stick-slip
- Measurement of internal cross-port bypass and external leakage
- Issuance of an official equipment technical passport (test certificate) detailing actual recorded test parameters
Frequently Asked Questions
How quickly do you repair hydraulic cylinders?
Turnaround times range from 5 to 45 business days, depending on the complexity of the repair and the scope of work. Large-bore and long-stroke cylinders may require additional lead time.
What if the piston rod is severely worn or damaged?
Turnaround times range from 5 to 45 business days, depending on the complexity of the repair and the scope of work. Large-bore and long-stroke cylinders may require additional lead time.
Can a cylinder be reconditioned if the barrel bore has deep scoring or gouges?
Turnaround times range from 5 to 45 business days, depending on the complexity of the repair and the scope of work. Large-bore and long-stroke cylinders may require additional lead time.
What types of seals do you use?
Turnaround times range from 5 to 45 business days, depending on the complexity of the repair and the scope of work. Large-bore and long-stroke cylinders may require additional lead time.
Do you perform in-house machining of replacement components for cylinder repairs?
Turnaround times range from 5 to 45 business days, depending on the complexity of the repair and the scope of work. Large-bore and long-stroke cylinders may require additional lead time.
Selected Heavy Cylinder Projects
Request Hydraulic Cylinder Repair Now
Attach a photo of the cylinder, an image of the nameplate (data plate) or describe the malfunction. Our specialist will contact you to clarify the technical details.